Both machines do the same job — move a torch at a constant speed — but they are guided in completely different ways. Get that distinction right and the choice is easy; get it wrong and you buy a machine that cannot reach the seam.
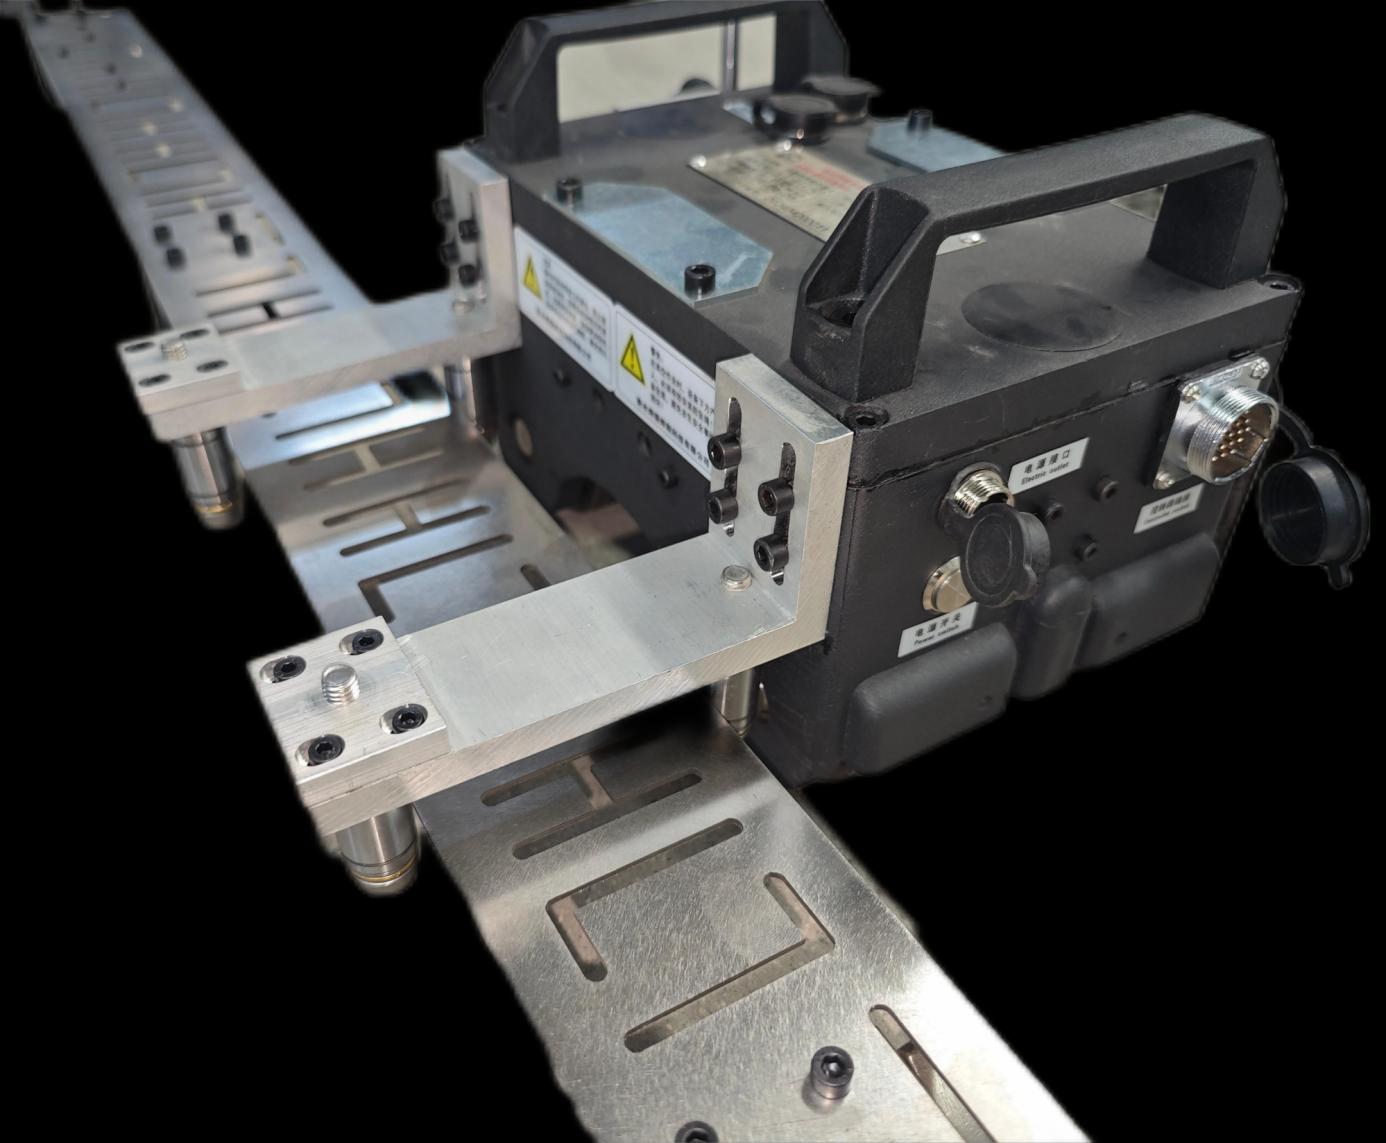
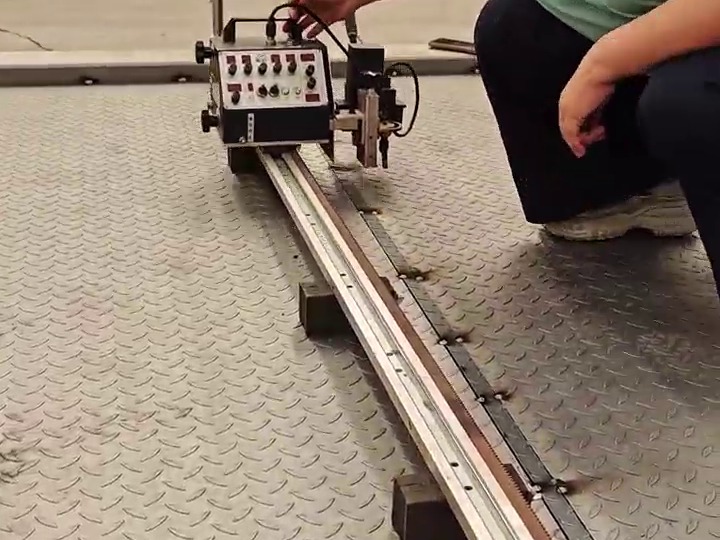
A welding carriage (what Europe and North America usually call a welding tractor or rail welding carriage) is guided by a track. The track is bolted, magnetically clamped or suction-mounted to the workpiece, and the carriage runs along it. The rail does the steering, so the torch path is straight by construction.
A crawler welding robot has no track at all. Magnetic wheels grip the steel directly and the machine drives itself along the joint. There is nothing to rig, which is why it reaches places a rail cannot: a finished tank shell, a pipe spool already sitting in its supports, the inside of a vessel.
That single difference explains almost every selection question we get. Speed, accuracy, minimum diameter and setup time all follow from it.
The honest version, including the jobs where neither machine is the answer.
| Job | Track-guided carriage (ZG / RG) | Crawler welding robot (CX) | Why |
|---|---|---|---|
| Long straight seams on flat plate | Best fit | Works, but slower | The rigid rail holds a true line at up to 1100 mm/min; the crawler is capped at 650 mm/min |
| Tank shell & circumferential seams | Flexible track (RG) follows the curve | Best fit | No track can be rigged on a finished shell — magnetic wheels just walk it |
| Pipe from Ø108 mm upward | Not possible | Only option | There is nothing to mount a rail on a 108 mm pipe |
| Curved plate and vessel bodies | RG flexible track, above Ø1800 mm | Best fit | The crawler needs no minimum diameter — it follows whatever it is standing on |
| H-beam and box-beam fillet welds | Trackless JJ / GJ fillet carriage | Not the right tool | Fillet welding needs a machine riding the corner at 45°, not a crawler |
| Vertical and overhead seams | Magnetic-track versions | Magnetic version only | What holds the torch is magnetic adhesion — that applies to both types |
| Very long or interrupted runs | Rails must be repositioned as you go | Less rigging time | Only matters if rigging time is your bottleneck — measure it before you pay for it |
| Thin sheet under 3 mm | Neither | Neither | Magnetic adhesion needs at least 3 mm of magnetically permeable material |
| Stainless and aluminium | Vacuum suction (/X) or clamping (/B) track | Magnetic version does not grip | No magnetic pull on non-ferrous metal — the track variant has to change |
| Small brackets and tight details | Manual | Manual | Access and setup time eat the gain; a carriage cannot pay for itself below a certain size |
If your shop does both long straight seams and curved or in-place work, the practical answer is often one of each rather than a compromise machine — the two are complementary, not competing.
We ask these in order. Whichever question returns a hard no stops the discussion — which saves you a quote for a machine that would not have worked.
If yes, a track-guided carriage wins on speed and line quality. Ask for ZG on flat plate, RG when the surface curves.
If it cannot be turned — a tank in place, a pipe spool in its supports — the crawler is the only option, because the rail has to sit on the workpiece.
The crawler welds pipe from Ø108 mm outer and Ø700 mm inner. The flexible track needs Ø1800 mm and above. Below those numbers the rail simply cannot conform.
Magnetic adhesion is the whole mechanism on vertical and overhead work. Stainless and aluminium need the vacuum-suction or clamping track variant instead.
Tell us the seam type, the workpiece size and whether the part can be turned — we will tell you straight whether a carriage or a crawler is the better buy for your shop.